Back to Ready Marketplace
Turnkey Plant
10 Months Payback
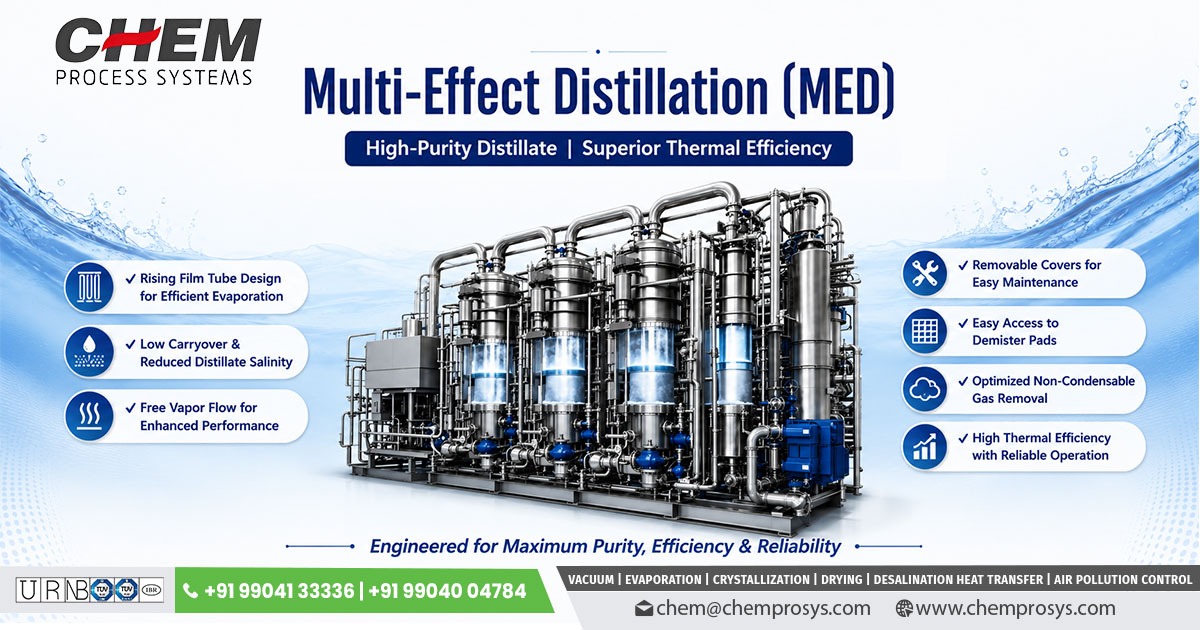
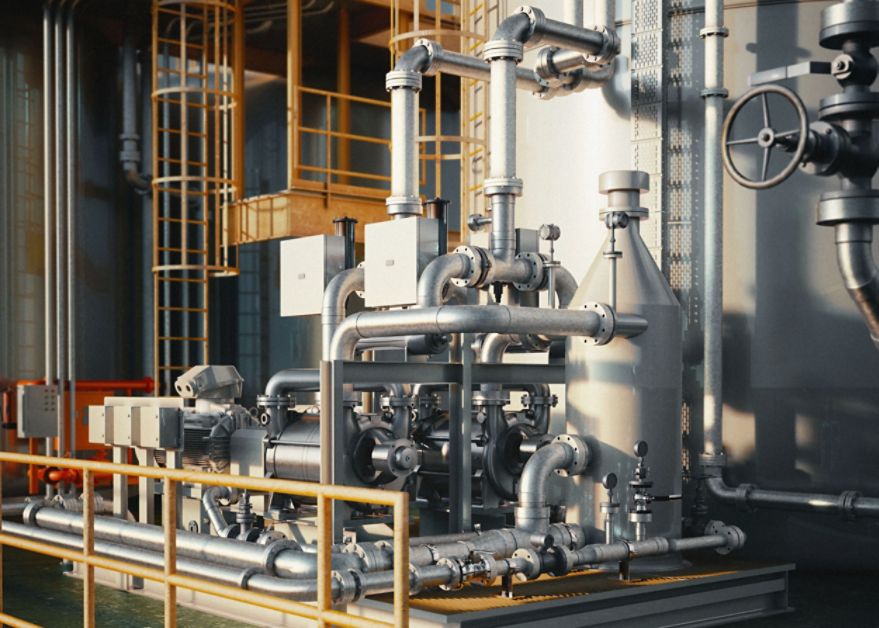
Multi Effect Distillation (MED) Plant
Dairy, Beverages & Breweries
•
Ahmedabad, Gujarat
Raw Material Contract
Handover Training
Machinery Loan / EMI
1 / 2
Model Type: Turnkey Plant
Full industrial machinery, site commissioning, tooling, and trial production batches ready for commercial deployment.
CapEx & Financial Viability
Base CapEx
₹25 L
Setup Outlay
Net Margin
33.0%
Est. Net Return
Payback
10 Mo.
Break-Even Target
Working Capital
₹5 L
Cushion Buffer
Rated Output Capacity: 10000 ltr/hr
Single Shift Model
Installation, Logistics & Recurring Costs
| Cost Element | Classification | Estimated Value |
|---|---|---|
| Installation & Commissioning | On-site foundation & engineering setup | Free (Included) |
| Transportation & Freight Charges | Transit logistics to buyer destination | On Actuals |
| Est. Monthly Raw Material Input | Input inventory per single shift run | Varies by Grade |
| Annual Maintenance Contract (AMC) | Post-warranty comprehensive support | Optional Support |
| Monthly Operator & Labor Payroll | Combined wage for required operators | Est. Based on Region |
| Guarantee / Warranty Period | Manufacturer direct terms | 1 Year Comprehensive Warranty |
Infrastructure & Plant Floor Footprint
2,000 sq.ft
Minimum Floor Area
60.00 KW
3-Phase Industrial
12 Personnel
Workforce / Shift
Raw Material Supplier Tie-Up Included
The seller facilitates direct mill/wholesaler pricing contracts for ongoing production runs.
On-Site Operator Technical Training
Vendor technical personnel oversee complete machine commissioning and operator handover.
Licensing & Government Subsidies
Statutory Clearances Required:
GST Registration
MSME / Udyam Certificate
Plant Blueprint & Deliverables Summary
In today’s competitive manufacturing industry, reducing energy consumption while achieving high-quality water recovery and wastewater concentration is essential.
A Multi Effect Distillation (MED) Plant is one of the most efficient technologies for industrial evaporation and distillation processes.
Chem Process Systems Pvt. Ltd. specializes in designing, manufacturing, supplying, installing, and commissioning Turnkey Multi Effect Distillation Plants that deliver maximum efficiency, operational reliability, and long-term cost savings for industries worldwide.
Whether you require a customized solution for pharmaceuticals, chemical processing, food & beverage, textile, or wastewater treatment, our engineering team delivers complete turnkey systems tailored to your production requirements.
A Multi Effect Distillation Plant (MED Plant) is an advanced thermal evaporation system where the vapor generated from one effect is reused as the heating medium for the next effect.
This significantly reduces steam consumption while maximizing water recovery and product concentration.
The technology is widely used for:
• Industrial wastewater treatment
• Solvent recovery
• Process water recovery
• Pharmaceutical purified water generation
• Chemical concentration
• Zero Liquid Discharge (ZLD) systems
• Effluent volume reduction
Advantages of Choosing Chem Process Systems Pvt. Ltd.
Complete Turnkey Execution
Single-source responsibility from engineering to commissioning.
Customized Engineering
Every project is designed according to client process requirements.
Energy-Efficient Solutions
Optimized steam consumption and lower operational costs.
Advanced Manufacturing Facility
Modern fabrication and strict quality control ensure reliable performance.
Experienced Engineering Team
Expertise in process engineering, automation, and project execution.
Reliable After-Sales Support
Comprehensive maintenance services, spare parts, and technical assistance.
Why Invest in a Turnkey Multi Effect Distillation Plant?
Investing in a turnkey MED plant provides significant long-term benefits:
• Reduced steam consumption
• Lower operating costs
• High return on investment (ROI)
• Improved production efficiency
• Environmental compliance
• Sustainable water management
• Reduced maintenance requirements
• Fully automated operation
• Faster project completion
• Reliable plant performance
Applications of Multi Effect Distillation Plant
• Process Water Purification
• Solvent Recovery
• Industrial Wastewater Concentration
• Pharmaceutical Water Systems
• High TDS Effluent Treatment
• Chemical Recovery
• Product Concentration
• Waste Volume Reduction
• Water Reuse Systems
• Zero Liquid Discharge Projects
FAQs:
What is a Multi Effect Distillation (MED) Plant?
A Multi Effect Distillation Plant is an energy-efficient system that reuses steam across multiple stages to reduce energy consumption while producing purified water or concentrating industrial liquids.
Which industries use Multi Effect Distillation Plants?
MED Plants are widely used in pharmaceutical, chemical, food processing, textile, distillery, power, and wastewater treatment industries.
What does a turnkey MED Plant solution include?
A turnkey solution covers engineering, design, manufacturing, installation, automation, commissioning, training, and after-sales support.
How does a MED Plant reduce operating costs?
It minimizes steam and energy consumption through heat recovery, resulting in lower utility costs and higher process efficiency.
Get a Complete Multi Effect Distillation Plant Turnkey Solution with Expert Design, Installation, and Support – Contact Us Today!
A Multi Effect Distillation (MED) Plant is one of the most efficient technologies for industrial evaporation and distillation processes.
Chem Process Systems Pvt. Ltd. specializes in designing, manufacturing, supplying, installing, and commissioning Turnkey Multi Effect Distillation Plants that deliver maximum efficiency, operational reliability, and long-term cost savings for industries worldwide.
Whether you require a customized solution for pharmaceuticals, chemical processing, food & beverage, textile, or wastewater treatment, our engineering team delivers complete turnkey systems tailored to your production requirements.
A Multi Effect Distillation Plant (MED Plant) is an advanced thermal evaporation system where the vapor generated from one effect is reused as the heating medium for the next effect.
This significantly reduces steam consumption while maximizing water recovery and product concentration.
The technology is widely used for:
• Industrial wastewater treatment
• Solvent recovery
• Process water recovery
• Pharmaceutical purified water generation
• Chemical concentration
• Zero Liquid Discharge (ZLD) systems
• Effluent volume reduction
Advantages of Choosing Chem Process Systems Pvt. Ltd.
Complete Turnkey Execution
Single-source responsibility from engineering to commissioning.
Customized Engineering
Every project is designed according to client process requirements.
Energy-Efficient Solutions
Optimized steam consumption and lower operational costs.
Advanced Manufacturing Facility
Modern fabrication and strict quality control ensure reliable performance.
Experienced Engineering Team
Expertise in process engineering, automation, and project execution.
Reliable After-Sales Support
Comprehensive maintenance services, spare parts, and technical assistance.
Why Invest in a Turnkey Multi Effect Distillation Plant?
Investing in a turnkey MED plant provides significant long-term benefits:
• Reduced steam consumption
• Lower operating costs
• High return on investment (ROI)
• Improved production efficiency
• Environmental compliance
• Sustainable water management
• Reduced maintenance requirements
• Fully automated operation
• Faster project completion
• Reliable plant performance
Applications of Multi Effect Distillation Plant
• Process Water Purification
• Solvent Recovery
• Industrial Wastewater Concentration
• Pharmaceutical Water Systems
• High TDS Effluent Treatment
• Chemical Recovery
• Product Concentration
• Waste Volume Reduction
• Water Reuse Systems
• Zero Liquid Discharge Projects
FAQs:
What is a Multi Effect Distillation (MED) Plant?
A Multi Effect Distillation Plant is an energy-efficient system that reuses steam across multiple stages to reduce energy consumption while producing purified water or concentrating industrial liquids.
Which industries use Multi Effect Distillation Plants?
MED Plants are widely used in pharmaceutical, chemical, food processing, textile, distillery, power, and wastewater treatment industries.
What does a turnkey MED Plant solution include?
A turnkey solution covers engineering, design, manufacturing, installation, automation, commissioning, training, and after-sales support.
How does a MED Plant reduce operating costs?
It minimizes steam and energy consumption through heat recovery, resulting in lower utility costs and higher process efficiency.
Get a Complete Multi Effect Distillation Plant Turnkey Solution with Expert Design, Installation, and Support – Contact Us Today!
ANYWORKS READY
Active Quotation
EMI / Machinery Loan
Available
Supported: Approved NBFCs & Banks
Request Full Blueprint & Demo
Direct manufacturer contact & NDA protected.
Jayesh Indravadan Parikh
Ahmedabad • Verified Plant Supplier
Recommended Alternatives
Similar Plant Blueprints & Machinery
Explore equivalent setups in Dairy, Beverages & Breweries and related turnkey categories.
Dairy, Beverages & Breweries
Gurgaon
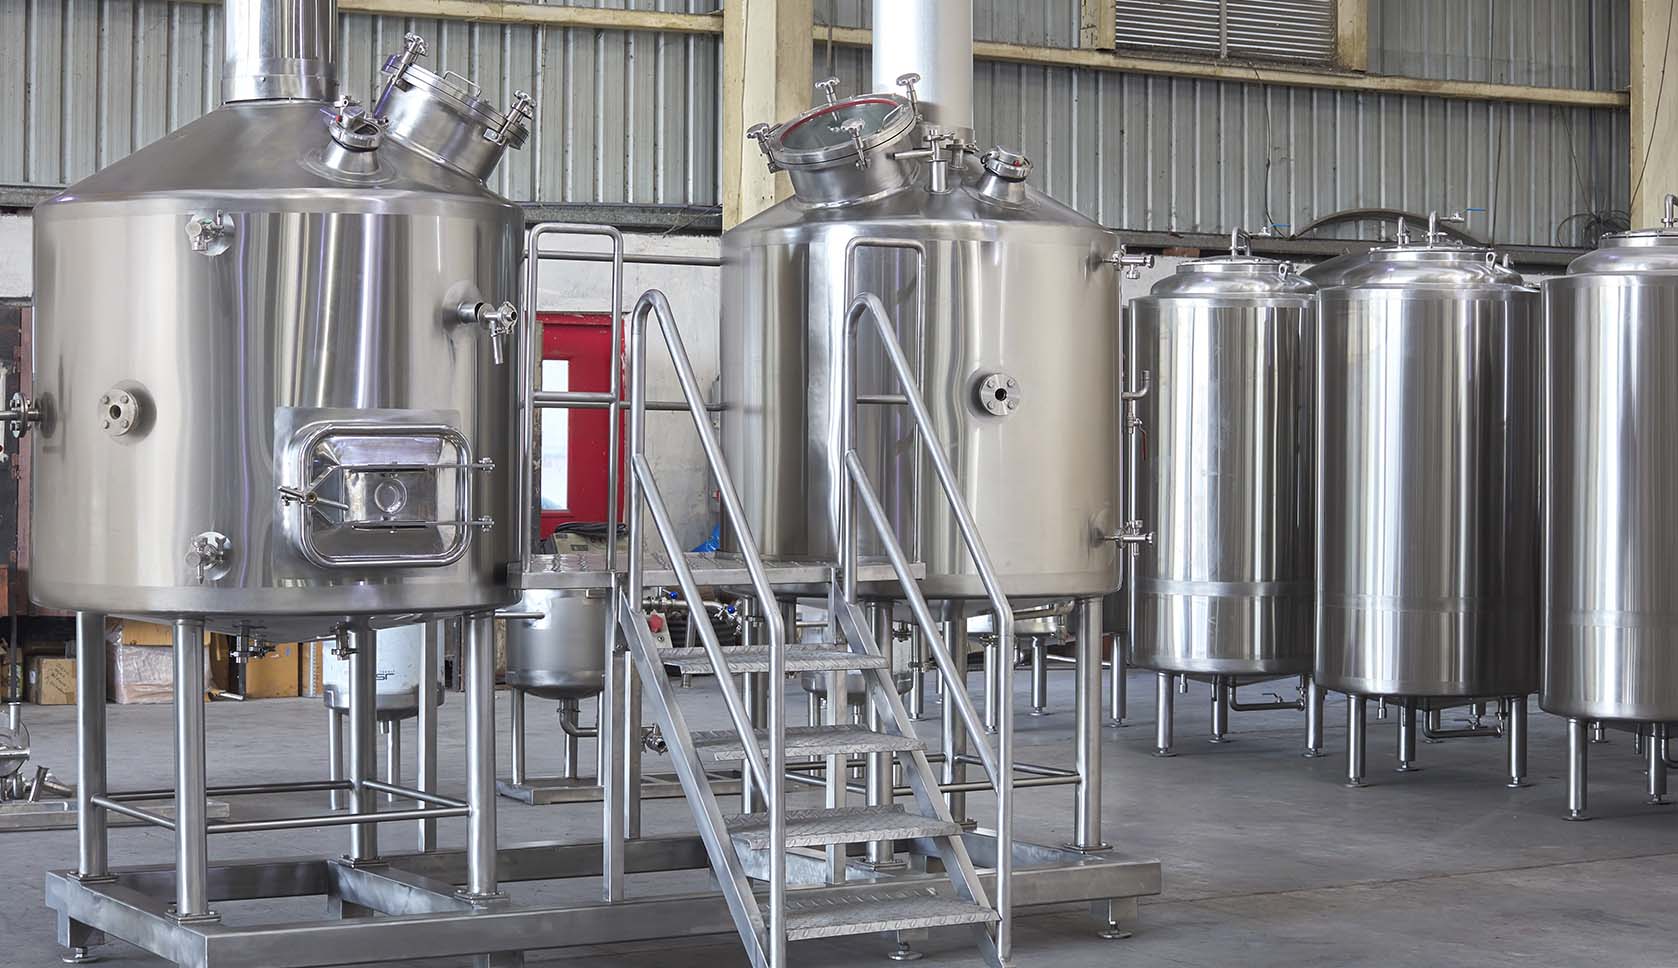
Beer Brewery Plant: Set It Up
Footprint: 1,200 sq.ft • 34.00 KW
Base CapEx
₹1,500,000
Net Margin
34.0%
Footwear
Tirupattur
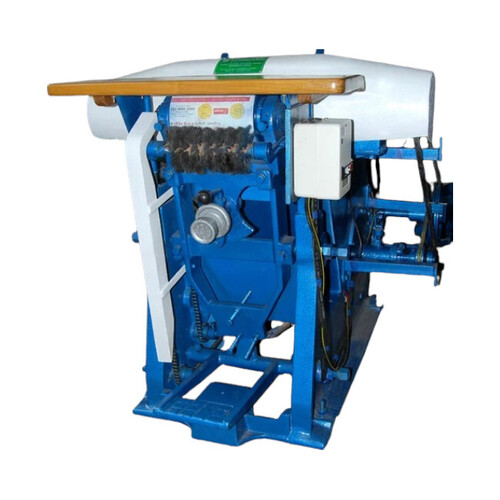
300mm Tannery Leather Buffing Machine
Footprint: 330 sq.ft • 25.00 KW
Base CapEx
₹275,000
Net Margin
22.0%
Infrastructure
Noida
Turnkey Paint Shop Manufacturer
Footprint: 3,000 sq.ft • 99.00 KW
Base CapEx
₹30,000,000
Net Margin
20.0%
Pharmaceuticals
Valsad
HTM PHARMA CAP (PLC)
Footprint: 500 sq.ft • 25.00 KW
Base CapEx
₹1,200,000
Net Margin
18.0%
House holds
New Delhi
Hydraulic Tile Making Machine
Footprint: 300 sq.ft • 12.00 KW
Base CapEx
₹850,000
Net Margin
25.0%
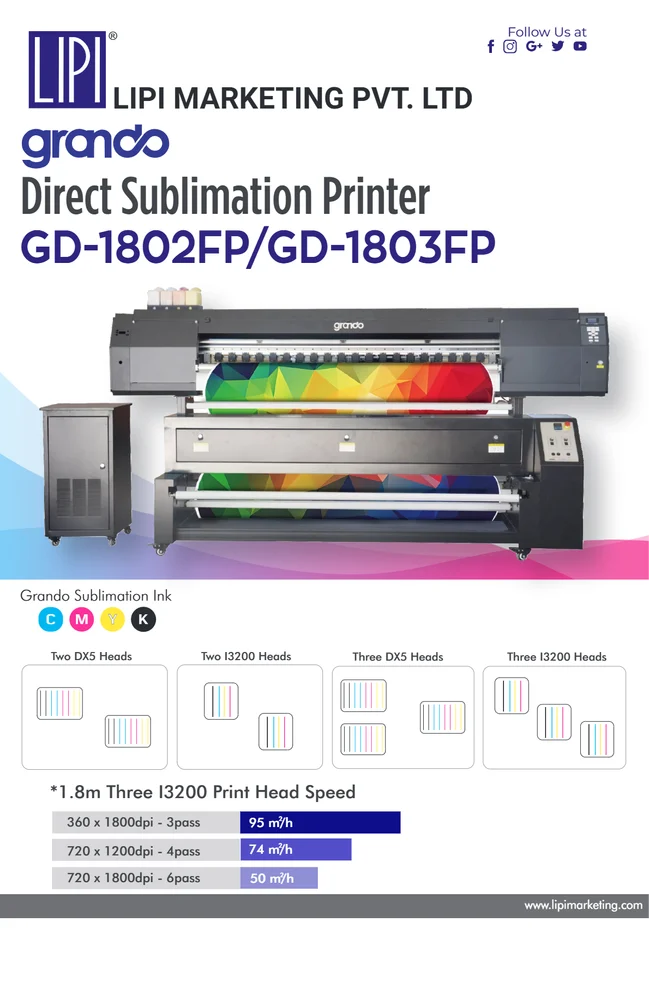
Printing & Signage
Chennai
Wide Format Dye Sublimation Printer, Flag Printing Machine
Footprint: 800 sq.ft • 25.00 KW
Base CapEx
₹1,200,000
Net Margin
35.0%